Introduction to Finned Tube Heat Exchangers
A Finned Tube Heat Exchanger is a highly efficient device designed to improve heat transfer between fluids or gases. It works by attaching fins to the outer surface of tubes, effectively increasing the heat transfer area. This design allows for faster and more efficient energy exchange, making finned tube heat exchangers ideal for various industrial heating and cooling processes.
In power plants and industrial boiler systems, finned tube heat exchangers play a crucial role in improving energy efficiency by recovering waste heat from exhaust gases. Among different fin types, H Finned Tubes are widely used due to their strong mechanical strength, compact structure, and excellent thermal performance.

What is an Economizer in Boiler
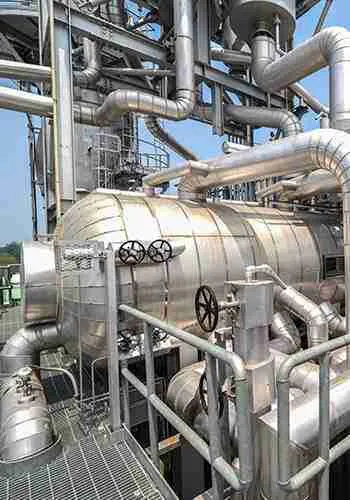
An economizer in boiler is a heat recovery device installed at the tail end of the flue gas path. Its main purpose is to utilize the residual heat in exhaust gases to preheat the boiler feed water before it enters the steam drum. This process reduces fuel consumption, lowers exhaust temperature, and significantly increases overall boiler efficiency.
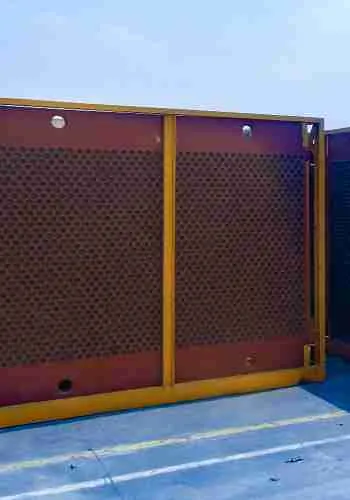
Structurally, a boiler economizer is a specific type of Finned Tube Heat Exchanger, designed to handle high-temperature flue gases and pressure conditions. The use of H Finned Tubes enhances heat exchange between the hot gas and the cooler feed water, making the system more energy-efficient and reliable.
Why Use H Finned Tubes in Boiler Economizers
H Finned Tubes are named for their “H-shaped” fins, which are welded symmetrically on both sides of the base tube. This design increases the heating surface area and strengthens the resistance to flue gas erosion. Compared with spiral finned tubes, H fins provide lower resistance, better soot-blowing performance, and longer operational life.
Advantages of H Finned Tubes in Boiler Economizers:
- High Heat Transfer Efficiency – The H-shaped fins expand the heat exchange area, improving the thermal efficiency of the economizer.
- Reduced Flue Gas Resistance – The special shape promotes smoother gas flow, reducing pressure drop.
- Improved Soot Blowing and Cleaning – The H structure prevents dust accumulation, maintaining long-term stable operation.
- Compact Design – The compact structure allows for easy installation and maintenance in limited spaces.
- Durability and Corrosion Resistance – The welded fins provide excellent mechanical stability, even under high-temperature and corrosive flue gas environments.

Manufacturing Process of Finned Tube Economizers
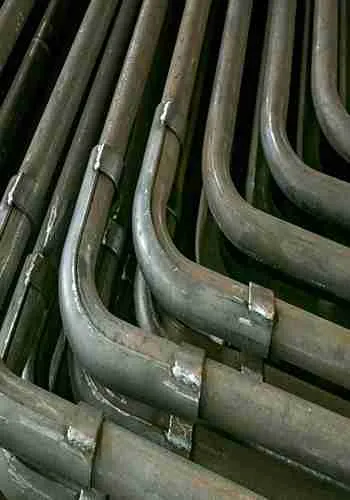
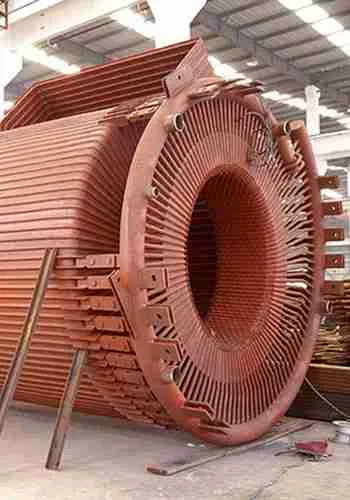
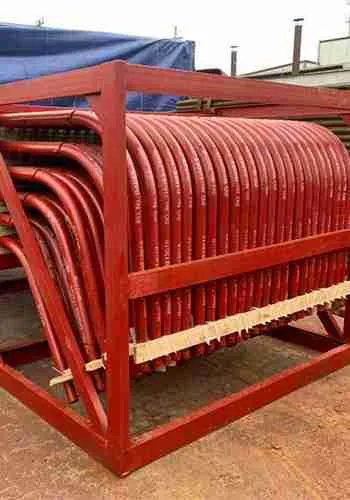
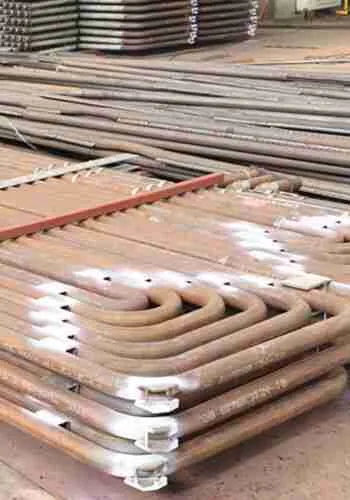
The economizer in boiler typically consists of a bundle of H Finned Tubes arranged in parallel rows. The manufacturing process includes:
- Tube Preparation – Selecting high-quality carbon steel or alloy steel tubes suitable for high-temperature operation.
- Fin Welding – Attaching H-shaped fins onto the tube surface through high-frequency resistance welding or laser welding to ensure strong bonding and good thermal contact.
- Assembly – Bundling the finned tubes into modules and connecting them with headers or manifolds for feedwater distribution.
- Inspection and Testing – Performing hydrostatic and air pressure tests to ensure leak-free operation.
- Surface Treatment – Applying anti-corrosion coatings to protect against oxidation and flue gas corrosion.
Applications of Finned Tube Heat Exchangers in Industrial Boilers
Finned tube heat exchangers, especially H Finned Tube Economizers, are essential components in:
- Coal-fired and Biomass Boilers – To recover heat from exhaust gases and improve overall thermal efficiency.
- Power Plants – To reduce fuel consumption and meet environmental emission standards.
- Industrial Heating Systems – For process heat recovery and energy saving in factories.
- Waste Heat Recovery Units – To utilize residual heat from furnaces, gas turbines, or exhaust systems.
Conclusion
The integration of Finned Tube Heat Exchangers in boiler systems—particularly in economizers in boilers—represents a key advancement in energy conservation technology.
By using H Finned Tubes, boiler manufacturers can achieve higher heat recovery efficiency, reduce fuel costs, and extend equipment lifespan.
At DHB Boilers, we design and manufacture high-performance H Finned Tube Economizers tailored for industrial and power generation applications, ensuring reliable operation and maximum energy savings.