Every boiler comes with a warranty—a one-year, two-year, or even five-year safety net that offers unwavering peace of mind. If a tube leaks, a weld cracks, or a control valve jams, a single phone call dispatches the supplier’s service team, who take full responsibility for the problem and its cost. For that period, reliability feels guaranteed.
Then the calendar turns, the warranty expires, and a profound silence sets in. But this silence is not empty—it is the quiet hum of metallurgical processes unfolding relentlessly, unseen and unannounced. Creep deformation accumulates along grain boundaries. Fatigue cracks take root at stress concentration points. High-temperature corrosion thins tube walls, micron by micron, day after day. These mechanisms do not recognize warranty deadlines, nor do they sound alarms. They simply progress, until one morning, the operator is jolted by a far different noise: the roar of an unplanned outage, the hiss of escaping steam, the urgent chaos of an emergency response.
This article pulls back the curtain on the hidden degradation that occurs inside boilers to 100,000 operating hours. For plant operators, EPC contractors, and project financiers, understanding these unseen processes is the critical difference between costly, unforeseen failures and controlled, predictable outcomes.
Part I: The Three Silent Killers
After a decade of service, every boiler component bears the invisible scars of its operational history. Three specific mechanisms determine whether a boiler reaches its twentieth year in sound condition—or fails catastrophically long before.
Creep: The Time-Dependent Deformation
At elevated temperatures, steel behaves dramatically differently than it does at room temperature. Above approximately 400°C, a slow, time-dependent deformation known as “creep” begins. In a superheater tube operating at 580°C, the alloy’s microstructure evolves gradually: fine carbide precipitates that pin grain boundaries coarsen, dislocations rearrange, and the tube elongates—imperceptibly at first, then measurably, until a bulge forms, a crack propagates, and the tube bursts.
The greatest challenge with creep is its invisibility. By the time visible deformation appears, the component has already consumed 90% of its useful life. Operators who rely solely on visual inspection are operating blindly, unaware of the irreversible damage unfolding beneath the surface.
Thermal Fatigue: The Damage of Every Startup
Every boiler startup and shutdown subjects its components to intense thermal stress. Temperature differences between adjacent sections—or between the inner and outer walls of a single tube—create strain that the material must absorb. Over thousands of cycles, this repeated strain accumulates into irreversible fatigue damage.
In modern power systems, where renewable energy intermittency forces conventional plants into daily load cycling, thermal fatigue has emerged as a primary threat. A boiler designed for base-load operation may now start and stop far more frequently than its designers anticipated, with each cycle consuming a small but cumulative fraction of the component’s fatigue life—faster than any nameplate rating would suggest.
Corrosion: The Chemical Thief
High-temperature corrosion operates like a thief in the night, eroding components without warning. In biomass-fired boilers, chlorine from agricultural residues attacks protective oxide layers, forming volatile metal chlorides that evaporate and leave fresh metal exposed. In coal-fired units, sulfur compounds condense on cooler surfaces, creating acidic deposits that eat through tube walls. In waste-to-energy plants, the toxic combination of chlorine, sulfur, and heavy metals creates a corrosive environment that challenges even the most advanced alloys.
Unlike creep and fatigue, corrosion leaves physical traces—wall thinning, pitting, and oxide scale formation—but detecting it requires more than visual inspection. Without precise wall thickness measurements, corrosion can thin a tube to the point of rupture while its external surface remains seemingly intact.
Part II: The Inspection Gap
Most plant operators conduct regular inspections, following manufacturer recommendations, complying with local regulations, and scheduling outages for visual examinations. Yet despite these efforts, tube failure-related forced outages remain the leading cause of unplanned downtime in thermal power plants.
The root cause? A fundamental gap in standard inspection protocols: they focus on what is visible, not what is happening beneath the surface.
Consider a typical superheater tube. A visual inspector might spot discoloration, slight bulging, or surface cracking—but the creep voids forming along grain boundaries (the true precursor to failure) are invisible to the naked eye. The oxide scale growing on the internal surface, which gradually insulates the metal and raises its operating temperature, cannot be seen from the outside. The fatigue microcracks initiating at tube-to-header welds are hidden beneath layers of scale and insulation.
This is the “inspection gap”: the disconnect between what operators can observe and what engineers need to know to prevent failure. Closing this gap requires moving beyond visual checks to embrace diagnostic technologies that reveal the boiler’s true internal condition.
Part III: The Data-Enabled Approach to Life Extension
The most sophisticated plant operators have abandoned the myth that inspections alone ensure reliability. Instead, they have adopted a data-enabled strategy that combines operational history, diagnostic measurements, and predictive modeling to extend boiler life while minimizing failure risk.
Baseline Establishment: Knowing Where You Started
Every life extension program begins with a baseline. Before a boiler enters service—or during its first major outage—operators should establish comprehensive dimensional and material records: wall thickness measurements at critical locations, hardness testing of key welds, and microstructural examination of representative samples. These baseline data points become the reference against which all future degradation is measured.
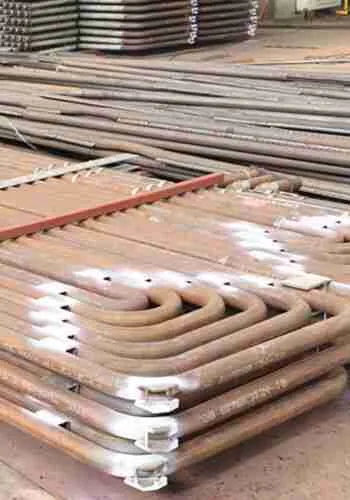
At DHB Boiler, we support our clients’ life extension efforts by providing detailed as-built documentation for every component we manufacture. Our 25-meter heat-treatment furnace, ISO 3834-2 certified welding systems, and rigorous inspection protocols ensure that when you receive a DHB superheater, you get not just a component, but a complete record of its initial condition—laying the foundation for decades of reliable monitoring.
Condition Monitoring: Tracking Degradation in Real Time
For critical components, periodic inspection is no longer sufficient. Leading operators are installing online monitoring systems that track key parameters continuously: wall temperature measurements identify areas where fouling or scale buildup is raising metal temperatures; acoustic emission sensors detect crack initiation before it becomes visible; vibration monitoring reveals changes in support conditions or flow-induced excitation.
These real-time data streams feed into diagnostic algorithms that alert operators to emerging problems—not after failure, but weeks or months in advance. This is the difference between reactive maintenance and true condition-based management: staying one step ahead of degradation, rather than scrambling to respond to breakdowns.
Remnant Life Assessment: Predicting the Future
The ultimate goal of life extension engineering is simple: to answer the question, “How much safe operating life remains?” Remnant life assessment combines all available data—design calculations, operational history, inspection results, and material testing—into a quantitative prediction of future performance.
For creep-dominated components, this means calculating the accumulated damage fraction using the Larson-Miller parameter or similar time-temperature correlations. For fatigue-limited locations, it involves counting cycles and summing damage according to Miner’s rule. For corrosion-affected areas, it means projecting future wall loss based on measured rates.
When these assessments indicate a component is approaching the end of its reliable life, operators have clear options: schedule replacement during a planned outage (avoiding the cost and chaos of emergency repairs), modify operating conditions to slow degradation (reducing temperature, limiting cycling, or adjusting fuel characteristics), or accept the risk with full transparency, knowing exactly how much margin remains.
Part IV: The DHB Commitment to Lifecycle Partnership
At DHB Boiler, we believe our responsibility to clients does not end when our equipment ships—it begins there. The warranty period is merely the formal expression of a commitment that extends across the entire operating life of every component we manufacture.
This commitment is tangible in our approach to design and documentation. When selecting materials, we prioritize long-term stability as much as initial performance. When specifying welding procedures, we document every parameter so future repairs can replicate the original, high-quality conditions. When conducting final inspections, we create records that serve as baselines for decades of future monitoring.
We have seen too many plants where operators discover—only after a costly failure—that their original equipment manufacturer provided no documentation, no guidance, and no support for life extension. The initial bid may have been low, but the long-term cost—unplanned outages, emergency repairs, and lost productivity—was devastating.
This is the paradox we strive to resolve. By investing in comprehensive documentation, rigorous quality systems, and ongoing technical support, we enable our clients to operate their boilers with confidence—not just during the warranty period, but for the decades that follow.
Conclusion: The 100,000-Hour Handshake
A boiler that reaches 100,000 operating hours is an extraordinary achievement. It has survived tens of thousands of thermal cycles, resisted the relentless advance of creep and corrosion, and delivered reliable steam day after day, year after year—through changing fuels, fluctuating loads, and evolving operating conditions.
That longevity is no accident. It is the product of sound initial design, disciplined manufacturing, and—most importantly—intelligent lifecycle management by operators who understand what happens after the warranty expires.
At DHB Boiler, we design and build for that 100,000-hour milestone. We engineer our components to degrade gracefully, to provide early warnings before failure, and to offer clear opportunities for life extension. We document our work thoroughly so that future engineers—people we may never meet—can understand what we created and make informed decisions about its continued service.
When you choose DHB, you are not simply buying equipment. You are entering a partnership that spans decades—a partnership that gives you access to the engineering knowledge, quality systems, and technical support needed to turn the 100,000-hour question from a source of anxiety into an opportunity for excellence.
The warranty expires. The partnership does not.